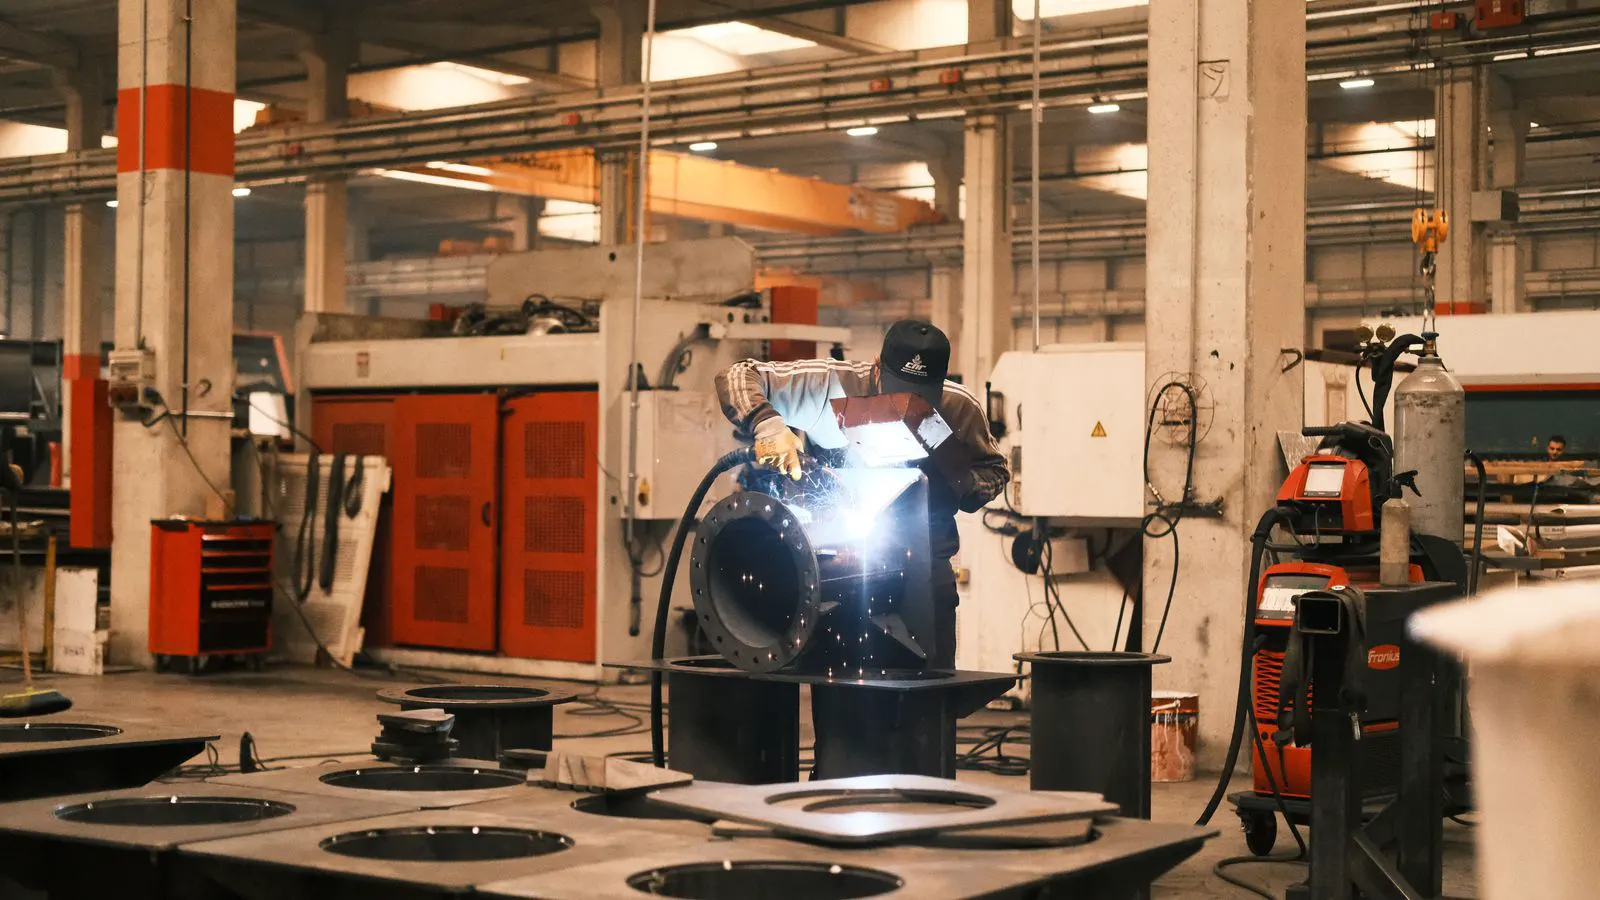
Spot welding joins parts at discrete points using high current, ideal for flat, thin sheet metal. Seam welding creates continuous welds for pressure vessels. Choose based on part geometry, material thickness, and required joint integrity.
- Spot welding is faster and cheaper for flat, thin sheet metal but creates weaker, non-continuous joints.
- Seam welding produces strong, continuous welds needed for pressure vessels and tanks.
- Use spot welding for automotive panels, appliance enclosures, and flat assemblies.
- Choose seam welding for tanks, boilers, and structures requiring full joint integrity.
- Material thickness and part geometry are the main deciding factors.
How Spot Welding Works
Spot welding joins two or more workpieces at discrete points. The machine clamps the parts together, then passes a high current through the workpiece for a short cycle. The resistance at the contact points generates heat, melting a small pool of metal. The molten core solidifies into a nugget that fuses the layers.
The process relies on electrode pressure. Too little pressure and the weld does not form. Too much pressure and the nugget crushes, creating a weak joint. Typical applications include automotive door panels, appliance housings, and flat metal assemblies.
The speed is high. One weld takes a fraction of a second. Multiple welds can be placed in minutes. The process runs on electricity only, with no filler wire or gas required. This makes it one of the most economical methods for thin sheet metal.
How Seam Welding Works
Seam welding creates a continuous weld along a joint. The workpieces are held in a fixture, and a continuous arc or resistance weld runs along the seam. In resistance seam welding, electrodes run along the joint while current flows through the metal. In arc seam welding, an arc melts the material continuously.
The result is a uniform weld bead that follows the joint line. This provides higher joint strength than spot welding. The weld can withstand internal pressure and mechanical stress along its full length.
The process is slower. The welder must maintain a steady travel speed. Fixtures must hold the parts in precise alignment. Any gap or misalignment causes defects. This method is common in tanks, boilers, and pressure vessels.
Spot Welding vs Seam Welding: Key Differences
| Option | Best for | Limitations |
|---|---|---|
| Spot welding | Thin sheet metal, flat assemblies, automotive panels, appliance enclosures | Weak joints, no pressure containment, limited to flat or nearly flat parts |
| Seam welding | Tanks, boilers, pressure vessels, continuous joint strength | Slower, requires precise fixtures, higher setup cost, limited to accessible seams |
| MIG welding | Medium thickness sheet, complex shapes, repair work | Slower than spot, requires filler and gas, heat distortion |
| TIG welding | Thin stainless, aluminum, high precision work | Very slow, expensive, requires skilled operator |
The table shows the core trade-offs. Spot welding wins on speed and cost for flat, thin parts. Seam welding wins on joint integrity for pressure applications. MIG and TIG fill the gap for parts that do not fit either category.
When to Choose Spot Welding
Pick spot welding when the part is flat or nearly flat. The electrodes must contact both surfaces. If the joint has a gap, the weld will not form. The material thickness matters too. Spot welding works best on thin to medium sheet metal. Thick plate requires different methods.
Automotive manufacturers use spot welding for body panels. The cars are flat sheet assemblies. The process runs fast on the production line. A single door can take hundreds of welds in minutes. The speed reduces labor cost. The welds are strong enough for the structural demands of the vehicle.
Appliance manufacturers use spot welding for refrigerator doors and oven panels. The parts are thin steel or aluminum. The welds are not load-bearing for the entire appliance. They hold the panels together while other fasteners handle the main load.
The main limitation is pressure. Spot welds are discrete points. They do not seal a joint against internal pressure. If you need to hold gas or liquid, spot welding is not the right choice.
When to Choose Seam Welding
Choose seam welding when the joint must be continuous. The weld runs the full length of the seam. This provides uniform strength. The joint can withstand internal pressure.
Tanks and boilers are the classic applications. The weld must be leak-tight. The material must be thick enough to handle the pressure. The fixture must hold the parts in exact alignment.
The process is slower. The welder must maintain a steady speed. If the speed changes, the weld quality changes. The heat input must be controlled. Too much heat causes burn-through. Too little heat causes a weak weld.
The setup cost is higher. The fixtures are more complex. The electrodes or arc must travel a long distance. The machine is more expensive than a spot welding station.
Material and Thickness Considerations
Material type affects the choice. Mild steel works well with both methods. Stainless steel is harder to weld. It requires more heat control. Spot welding works on stainless, but the nugget quality is more sensitive to pressure and current. Seam welding on stainless requires careful heat input to avoid distortion.
Aluminum is more challenging. It has low melting point and high thermal conductivity. Spot welding works on aluminum, but the electrodes must be designed for it. Seam welding on aluminum requires special electrodes or arc methods.
Thickness is the main factor. Thin sheet metal favors spot welding. The heat is localized. The process is fast. The distortion is low. Thick plate favors seam welding or other methods. Spot welding cannot penetrate thick material. The nugget would be too small.
Fixtures and Setup
Both methods require fixtures. The parts must be held in position. The electrodes or arc must access the joint.
For spot welding, the fixture holds the parts flat. The electrodes press down on the joint. The fixture must allow the electrodes to reach every weld point. The parts must be clean. Paint, oil, or rust prevent proper contact.
For seam welding, the fixture holds the parts in exact alignment. The joint must be tight. Any gap causes defects. The fixture must allow the electrodes or arc to travel the full length. The fixture must be rigid. Any movement during welding causes defects.
The setup time for spot welding is shorter. The fixtures are simpler. The electrodes are stationary. The parts are clamped, and the machine fires the welds.
The setup time for seam welding is longer. The fixtures are more complex. The electrodes or arc must be aligned. The travel path must be programmed. The parts must be held perfectly still.
Cost and Production Speed
Spot welding is faster and cheaper. The cycle time is short. The machine can fire multiple welds in parallel. The labor cost is low. The machine cost is low.
Seam welding is slower and more expensive. The cycle time is long. The machine must travel the full length of the joint. The labor cost is higher. The machine cost is higher.
For high volume production, spot welding is the clear winner. The speed reduces the cost per part. The automation potential is high. The process is easy to integrate into a production line.
For low volume or high value parts, seam welding may be justified. The joint strength is critical. The cost of failure is high. The slower process is acceptable.
Common Mistakes to Avoid
The most common mistake is using spot welding for pressure applications. The welds are not continuous. They will leak. The part will fail under pressure.
The second mistake is poor fixture design. If the parts move during welding, the weld will be weak. The fixture must be rigid. The parts must be clean.
The third mistake is incorrect electrode pressure. Too little pressure causes a small nugget. Too much pressure crushes the nugget. Both create weak joints.
The fourth mistake is ignoring material thickness. Spot welding does not work on thick plate. Seam welding does not work on very thin sheet without burn-through.
The fifth mistake is not checking the weld. Visual inspection is not enough. The weld must be tested. For pressure applications, hydrostatic testing is required. For structural applications, non-destructive testing may be needed.
Final Selection Guide
The choice between spot and seam welding depends on the part. Ask these questions.
- Is the part flat or nearly flat? Spot welding works best on flat parts. Seam welding works on curved and complex shapes.
- Does the part need to hold pressure? Seam welding is required. Spot welding will leak.
- What is the material thickness? Thin sheet favors spot welding. Thick plate favors seam welding or other methods.
- What is the production volume? High volume favors spot welding. Low volume favors seam welding if joint strength is critical.
- What is the joint geometry? Straight seams favor seam welding. Irregular shapes favor spot welding or other methods.
The answer is usually obvious. Flat, thin, high volume parts use spot welding. Pressure vessels and tanks use seam welding. Medium thickness, complex shapes, and low volume parts may need MIG or TIG welding.
The key is to match the method to the function. Do not choose a method based on cost alone. Do not choose a method based on speed alone. Choose the method that meets the functional requirements of the part.
Frequently asked questions
Can spot welding be used for pressure vessels?
No. Spot welds are discrete points and do not seal a joint against internal pressure. Seam welding is required for pressure vessels.
What is the maximum thickness for spot welding?
Spot welding works best on thin to medium sheet metal. Thick plate requires other methods because the nugget cannot penetrate the full thickness.
Is seam welding faster than spot welding?
No. Seam welding is slower because the weld runs the full length of the joint. Spot welding fires discrete welds in a fraction of a second.
Can you mix spot and seam welding on the same part?
Yes. Some parts use both. The seam weld provides the main strength, and spot welds hold the parts together during fabrication.
What happens if the sheet is dirty during spot welding?
The weld will not form properly. Paint, oil, or rust prevent electrical contact. The metal must be clean and flat for a good weld.


