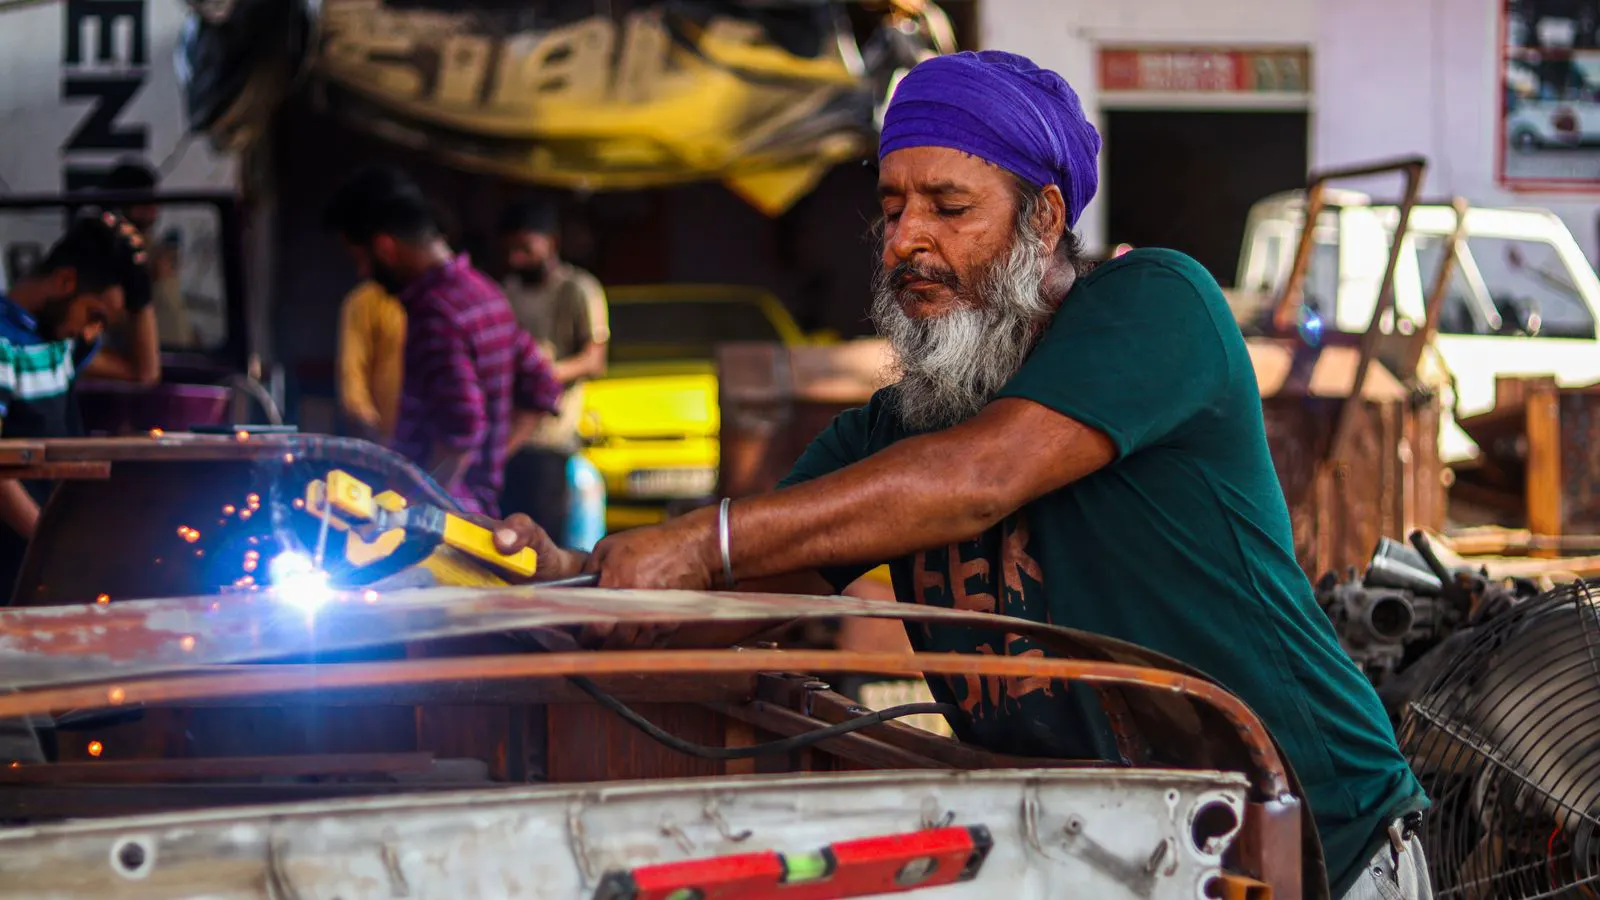
Verify welder qualifications by checking certification records against specific materials and processes. Confirm the welder has passed tests for your exact alloy, thickness, and joint configuration. Review fit-up and shielding gas records.
- Match the welder certification to the specific material, thickness, and joint type in your drawing.
- Request certification records that include the date, process, and base metal used for the test coupon.
- Perform a visual inspection of recent work to check for consistent bead profile and clean fit-up.
- Ask for shielding gas flow rates and wire feed speed settings used on similar sheet metal projects.
- Flag any discrepancies between the advertised capability and the documented test results.
Confirm the Certification Matches Your Material
The first step in any welder audit is verifying that the certification covers the exact material you are supplying. A welder certified for mild steel does not automatically qualify to weld 304 stainless. The base metal chemistry changes the required preheat, the shielding gas mix, and the filler metal selection.
Ask the fabricator for the specific certification number and the issuing body. If they only provide a generic “qualified” statement, that is a red flag. You need to see the test coupon details. The record should state the base metal grade, such as A36 or 304L. It should also list the thickness range covered by the test. A welder qualified for 12 to 16 gauge sheet may not be qualified for 4 or 5 gauge stock. The heat input requirements differ significantly at those thinner sections.
Check the process used for the certification. TIG and MIG require separate qualifications. A welder who passed a TIG test on stainless cannot claim a MIG qualification for the same alloy unless the records show a distinct test for the MIG process. If your drawing calls for MIG on the primary joints and TIG on the cosmetic edges, the fabricator needs welders qualified for both processes on your specific material.
Check the Joint Configuration and Position
Sheet metal jobs often involve specific joint geometries. The certification must reflect the joint type you are using. A T-joint requires different heat control than a butt joint. A lap joint with a single fillet weld has different requirements than a double fillet.
Look at the joint configuration in the certification record. If the record says “butt joint, flat position,” and your assembly requires a vertical or horizontal T-joint, the qualification may not apply. For thin sheet metal, position is less of a constraint for the welder’s hand stability, but it is still a factor in heat distortion management.
The thickness range in the certification is just as critical. If the fabricator is qualified for 1/8 to 1/4 inch plate, they may not be qualified for 18 gauge sheet. The gap between the sheets in a T-joint is different. The penetration depth required is different. The risk of burn-through is higher in thinner stock. Ask them to explain how their qualified thickness range covers your specific stock. If they cannot show a test coupon for a thickness close to yours, that is a gap in their qualification.
Review the Shielding Gas and Filler Metal Records
Shielding gas is not a one-size-fits-all choice. For stainless steel, the gas mix is typically 90% argon and 10% CO2, or a 75% argon, 15% CO2, and 10% helium blend. For mild steel, it is often 75% argon and 25% CO2. The specific mix matters for arc stability and bead appearance.
Ask for the shielding gas flow rate used on the test coupon. A low flow rate can cause porosity. A high flow rate can pull in air if the setup is not shielded correctly. For TIG on stainless, the flow rate is usually in the range of 10 to 20 cubic feet per hour. For MIG, it is higher, often 20 to 30 cubic feet per hour. If the fabricator cannot provide these numbers, they are not tracking their process parameters.
Filler metal selection is also part of the qualification. The welder must use the correct filler for the base metal. For 304 stainless, ER308L is the standard filler. For 316, it is ER316L. For mild steel, ER70S-6 is common. Ask them to confirm the filler wire used in their qualification test. If they use the wrong filler, the weld will fail even if the technique is sound.
Perform a Visual Welder Audit of Recent Work
Paperwork is one thing. The actual welds are another. Request a visual audit of the most recent sheet metal assemblies they produced. Look at the welds on the edges of the panels. Check the bead profile. A good TIG weld on sheet metal should have a smooth, even stringer or a consistent ripple pattern. There should be no undercut, no porosity, and no excessive spatter.
For MIG welds, look for the stack of dimes profile. The beads should be uniform in height and width. If the beads are too tall, the heat input is too high. If they are too flat, the wire feed speed may be too low. Check the fit-up. The edges should be clean and close together. Gaps larger than 1/16 inch are difficult to weld in sheet metal without distortion.
Look for distortion. Thin sheet metal warps easily. If the panels are twisted or the angles are off, the welder did not manage the heat input correctly. This is a direct result of poor qualification or improper technique. A qualified welder on sheet metal should use techniques like pulse welding or low travel speed to minimize heat. If their recent work shows significant warp, their qualification may be theoretical, not practical.
Verify the Preheat and Interpass Temperature Controls
Preheat is rarely used on thin sheet metal, but it is sometimes required for thicker sections or certain alloys. Interpass temperature is more relevant. If a joint requires multiple passes, the temperature between passes must be controlled. For stainless steel, keeping the interpass temperature below 250 degrees Fahrenheit prevents sensitization and reduces cracking.
Ask the fabricator how they control interpass temperature. Do they use an infrared thermometer? Do they rely on touch? Touch is not reliable. Infrared is better. For high-strength alloys like 300 series stainless, temperature control is critical. If they cannot explain their method, they are likely relying on guesswork. This is a red flag for a welder audit.
Check if they use a backing bar. For TIG welds on the back side of the joint, a copper backing bar is often used to control the back bead and prevent burn-through. If the fabrication area shows no backing bars, and the back side of the weld is visible, ask how they maintain penetration. For sheet metal, the back side is often left rough or ground, but it must be sound.
Confirm the Welder Audit Documentation
The final step is to ensure the documentation is complete and current. Welder qualifications expire. Most certifications are valid for six months from the date of the test. Ask for the date of the last test. If the date is older than six months, the welder is not currently qualified.
Request a copy of the test report. It should include the date, the welder ID, the process, the base metal, the filler metal, the shielding gas, the thickness, and the joint configuration. If any of these details are missing, the qualification is incomplete. You need a complete record to verify their capability.
Keep a log of these audits. If you order from multiple fabricators, maintain a database of their welder qualifications. This makes future RFQs faster. You can ask them to provide their current certification records as part of the proposal. This shifts the burden to the vendor and ensures you are not relying on verbal assurances.
Common Red Flags in Welder Qualification
| Red Flag | Why It Matters | Action |
|---|---|---|
| Generic “qualified” statement | Does not specify material or process | Request detailed certification record |
| Certification older than 6 months | Qualification has expired | Ask for re-test or new welder |
| Thickness range does not match | Heat input and gap differ | Reject if no matching test coupon |
| No shielding gas flow rate given | Cannot verify arc stability | Ask for process parameter sheet |
| Visible weld distortion | Poor heat management | Audit recent work for warp |
| Wrong filler metal used | Weld may crack or fail | Verify filler for base metal |
If you see any of these red flags, do not proceed. Ask for a re-test or a second welder. Do not accept “we have done this before” as an answer. Qualification is a documented fact. It is not a claim.
Final Verification Steps
Before releasing the work order, run the final verification. Check the certification number against the issuing body if possible. Verify the welder name matches the name on the crew sheet. Confirm the material lot number matches the base metal in the drawing.
Send a copy of this checklist to the fabricator. Ask them to complete it for each welder assigned to your job. This creates a shared responsibility. It shows you care about quality. It also gives them a clear standard to meet.
If they refuse to provide the documentation, that is your answer. A fabricator that hides their welder qualifications is hiding a weakness. Move on to a vendor that is willing to show their work. The cost of a bad weld is higher than the cost of verifying a good welder.
The goal is to match the welder to the job. The job is the material, the thickness, the joint, and the process. If the welder is qualified for that specific combination, you are covered. If not, you are taking a risk. This checklist removes that risk.
Use this checklist for every sheet metal welding project. Do not skip steps because the project is small. Even a small bracket can fail if the welder is not qualified for the thickness or the material. The cost of a rework is low compared to the cost of a failed assembly.
The audit is quick. It takes ten minutes to check the paperwork. It takes twenty minutes to look at the welds. It takes five minutes to verify the gas mix. The total time is less than an hour. That hour saves you days of trouble.
Do not rely on the vendor’s reputation. Reputation is built over time. Certification is verified today. Use the certification. Use the audit. Use the checklist.
This is how you verify a sheet metal welder qualification. You check the paper. You check the weld. You check the process. You check the date. You check the material. You check the joint. You check the gas. You check the filler. You check the temperature. You check the distortion.
You are not guessing. You are verifying. That is the difference between a good weld and a bad weld. That is the difference between a satisfied customer and a returned part.
Use this checklist. Save it. Print it. Keep it in your folder. Use it for every RFQ. Use it for every PO. Use it for every welder.
The welder is the last line of defense. The drawing is the first line. The material is the second line. The fit-up is the third line. The welder is the fourth line. If the fourth line is weak, the whole structure is weak.
Verify the fourth line. Every time. Without exception.
Frequently asked questions
Does a TIG qualification cover MIG work?
No, TIG and MIG are separate processes with different heat input and arc characteristics. A welder must be qualified for each process individually.
How often does a welder qualification expire?
Most standard qualifications are valid for six months from the date of the test coupon. After that, a re-test is required.
Can a welder qualified for plate weld sheet metal?
Not necessarily. The thickness range in the qualification must cover your specific stock. Plate qualification does not automatically cover thin sheet.
What is the most common gas mix for stainless?
For stainless steel, a mix of 90% argon and 10% CO2 is common. Some shops use 75% argon, 15% CO2, and 10% helium.
Do I need to see the welder ID?
Yes, the welder ID should match the certification record. This ensures the person welding is the person qualified.