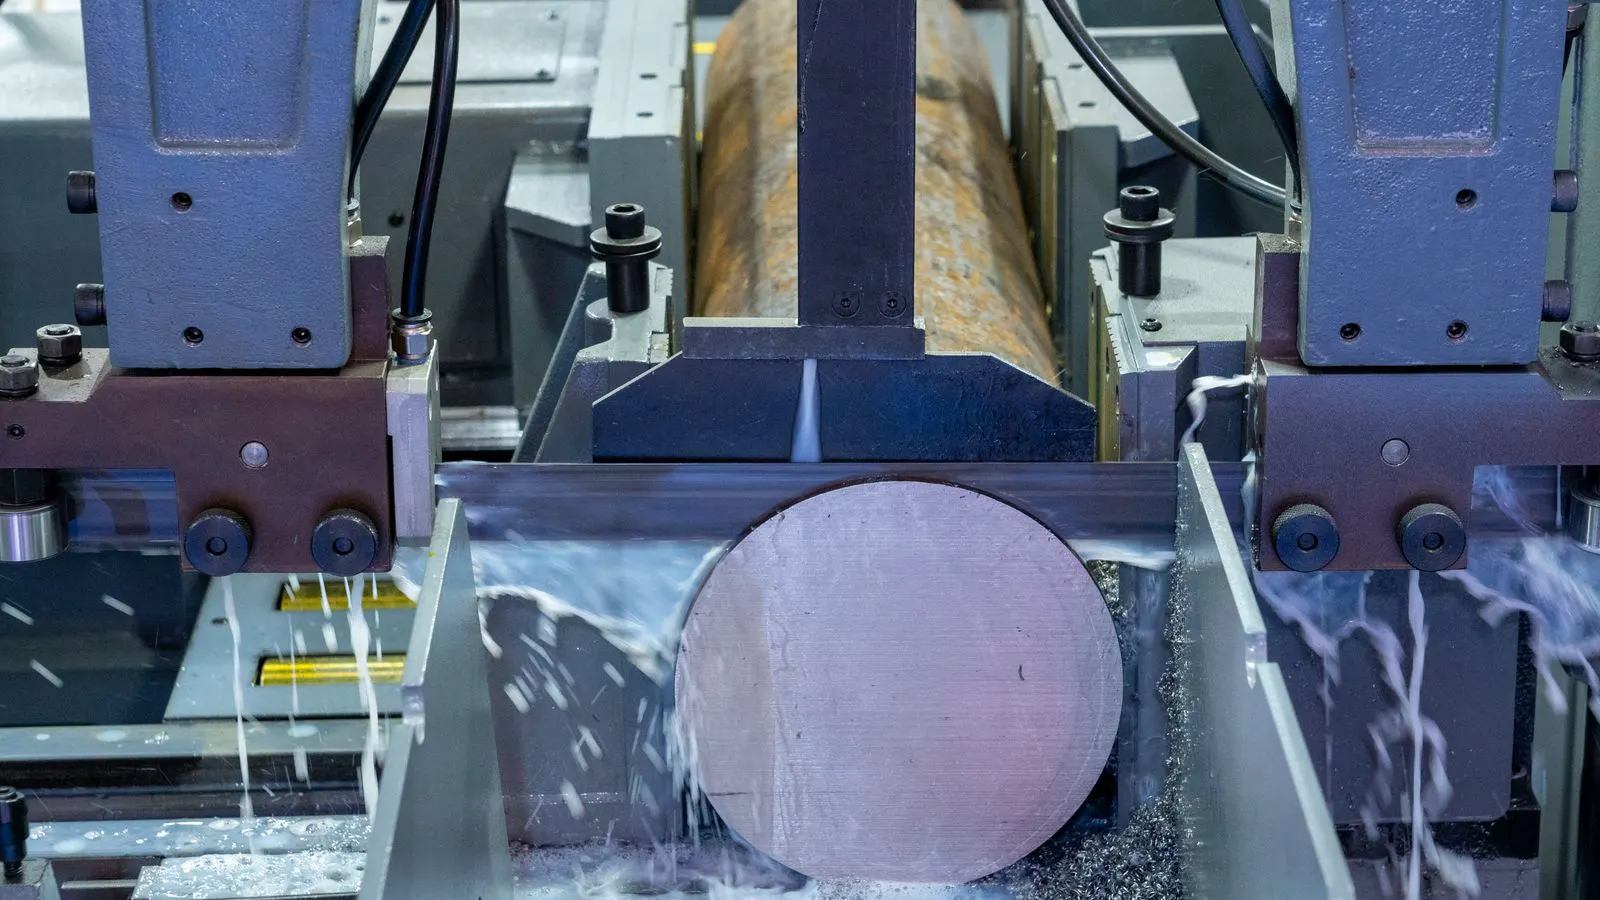
Choose waterjet cutting over plasma when heat-affected zones or corrosion are unacceptable. This guide outlines the specific scenarios where waterjet is preferred, the preparation required, and how to manage the operational shifts it introduces to your fabrication workflow.
- Waterjet is the preferred method when thermal cutting creates unacceptable heat-affected zones or corrosion.
- Buying waterjet capability requires planning for specific workflow shifts, including material handling and waste management.
- Preparation involves selecting the right nozzles and verifying the material type to ensure the waterjet is the correct tool.
When Does Corrosion Force a Change in Strategy?
Many professional buyers and engineers face a common dilemma in sheet metal fabrication: the need for precision without the side effects of heat. While thermal methods are often the first choice for speed and cost efficiency, they introduce a heat-affected zone (HAZ) that can compromise material integrity. For certain applications, such as food-grade stainless steel, aerospace components, or chemical processing tanks, this HAZ can lead to oxidation, warping, or corrosion. In these cases, understanding the difference between plasma cutting vs waterjet is essential for maintaining product quality and meeting strict regulatory standards.
Waterjet cutting is a non-thermal process that uses a high-pressure stream of water, often mixed with an abrasive particle, to slice through metal. Because no flame or electric arc is involved, the material is not subjected to the high temperatures that cause heat-affected zones. This makes it the ideal solution for corrosion-free cutting, particularly when working with sensitive alloys or when the final surface finish is critical.
How Does Waterjet Cutting Sheet Metal Differ from Thermal Methods?
The primary difference lies in the mechanism of cutting. Plasma cutting uses an ionized gas stream to melt and blow away the metal. This process is fast and effective for thicker materials but inevitably leaves a rough, oxidized edge. Waterjet, by contrast, mechanically removes material. It does not melt the sheet; it shears it.
This mechanical action means that the edge quality of the cut can be superior, especially in thin to medium gauges. However, the speed of a waterjet is generally slower than that of a plasma cutter. Therefore, the decision is rarely about speed alone. It is a trade-off between processing time and material preservation. If the cost of reworking a plasma-cut part due to corrosion or warping exceeds the extra time spent on a waterjet cut, the waterjet is the more economical choice in the long run.
What Are the Five to Six Shifts Buyers Should Plan For?
Integrating waterjet cutting into your fabrication workflow is not just about adding a machine; it is about shifting how your team operates. Buyers and engineers should plan for the following operational changes to ensure a smooth transition and maximize the benefits of corrosion-free cutting.
- Material Handling and Fixturing: Waterjets require precise clamping to hold the sheet in place against the high-pressure stream. Unlike plasma, where the heat can sometimes help hold a loose sheet, a waterjet needs a solid bed. You will need a dedicated, flat, non-slip cutting bed that can accommodate the specific size of your sheets.
- Nozzle Management and Maintenance: The abrasive waterjet nozzle wears down with every cut. This requires a systematic maintenance schedule. You must plan for the cost and availability of replacement nozzles, which are significantly more expensive than plasma tips.
- Waste and Water Management: Waterjet cutting generates a significant amount of water and slurry. You will need a plan for draining and filtering this waste. In many facilities, this requires a dedicated sump and filtration system to prevent clogging the pipes and to comply with local environmental regulations.
- Speed Expectations: Teams used to the speed of plasma cutting may be surprised by the slower feed rate of a waterjet. Production schedules must be adjusted to reflect this. If a job is time-critical, a waterjet may not be the right tool, even if it is the best for quality.
- Edge Quality Verification: Because waterjet cuts do not have the same thermal distortion, the edges are often cleaner. However, the cut width can vary depending on the abrasive and pressure settings. It is important to verify the edge quality after the first few parts of a new job to ensure it meets your tolerance needs.
- Cost of Operation: The cost of a waterjet cut is often higher per hour than plasma. This is due to the cost of abrasive, water, and electricity. When calculating the cost of a job, you must factor in this higher operating cost and weigh it against the value of a clean, corrosion-free edge.
How to Prepare Your Facility for Corrosion-Free Cutting
Preparing your facility for waterjet cutting requires attention to detail. Before you install a machine or outsource the work, ensure your setup can support the process.
Verify the Material
Not all materials are suitable for waterjet. While waterjet can cut a wide variety of metals, including steel, aluminum, and stainless steel, it is also used for non-metals like rubber and plastic. However, for sheet metal fabrication, the focus is usually on metals. Ensure the material you are cutting is within the machine’s capability. Very thin metals, for example, can be difficult to cut without warping or being displaced by the pressure.
Select the Right Nozzle
The nozzle is the heart of the waterjet. It is available in various sizes and materials. A smaller nozzle provides a finer cut but wears out faster. A larger nozzle is faster but produces a wider cut. You must select the nozzle based on the material thickness and the desired edge quality. For corrosion-free cutting, the edge quality is paramount, so you may need to invest in higher-quality nozzles that maintain their precision longer.
Ensure Adequate Power and Water Supply
Waterjets require a consistent supply of high-pressure water and often a reliable power source for the pumps. You need to verify that your facility’s water pressure and power capacity can support the machine. In some cases, you may need to install a dedicated pump or upgrade your electrical system.
How to Evaluate Waterjet for Your Specific Project
When deciding whether to use waterjet or plasma for a specific project, consider the following factors:
| Factor | Plasma Cutting | Waterjet Cutting |
|---|---|---|
| Heat-Affected Zone | High; can cause corrosion | None; corrosion-free cut |
| Speed | Fast | Slower |
| Cost | Lower per hour | Higher per hour |
| Edge Quality | Rough; requires grinding | Fine; often ready for welding |
| Material Limit | Limited by thickness | Can cut thicker materials |
| Best For | Thick steel, speed | Precision, sensitive alloys |
If your project involves stainless steel for food processing, a waterjet is often the only viable option. The thermal damage from plasma can lead to pitting corrosion, which is unacceptable in such environments. Similarly, if you are cutting thin aluminum for a cosmetic application, the waterjet’s precision and lack of heat distortion will result in a higher-quality finish.
However, if you are cutting thick structural steel where speed and cost are the primary concerns, plasma may be the better choice. The heat-affected zone in structural steel is often less critical, and the speed advantage of plasma can make it the more economical option.
Final Thoughts: Choosing the Right Cut
The decision between plasma cutting vs waterjet is not a one-size-fits-all choice. It is a strategic decision based on the specific requirements of your project. For corrosion-free cutting, waterjet is the preferred method. It eliminates the heat-affected zone and provides a clean, precise edge that is ideal for sensitive materials and applications.
To make the most of a waterjet, you must plan for the operational shifts it brings. From material handling to waste management, these changes require preparation and investment. By understanding these factors and preparing your facility accordingly, you can ensure that the waterjet delivers the quality and reliability your projects demand. For many professional buyers and engineers, the investment in waterjet capability is justified by the ability to take on higher-value, precision-driven work that thermal cutting cannot match.
Frequently asked questions
Is waterjet cutting always better than plasma cutting?
No, waterjet is not always better. It is slower and more expensive per hour than plasma. Plasma is often the better choice for thick materials where speed and cost are prioritized over edge quality.
What is a heat-affected zone (HAZ)?
A heat-affected zone is the area of metal that is changed by the high heat of thermal cutting processes like plasma or laser. It can cause oxidation, warping, or corrosion in sensitive materials.
Can waterjet cut all types of sheet metal?
Waterjet can cut a wide variety of metals, including steel, aluminum, and stainless steel. However, very thin metals can be difficult to cut without warping, so it is important to test the material before production.
How much does waterjet cutting cost compared to plasma?
Waterjet cutting is generally more expensive per hour than plasma cutting due to the cost of abrasive, water, and electricity. However, the higher quality of the cut can reduce the need for secondary operations like grinding, which can save money overall.
What is the main advantage of waterjet cutting for corrosion-free applications?
The main advantage is that it is a non-thermal process. Because it does not use heat, it does not create a heat-affected zone, which means the metal is not oxidized or corroded by the cutting process.


